Large Equipment Does Not Always Need to Lead the Layout
Large equipment can still fit into a layout-first process when its position remains flexible. A floor-standing product may have several workable locations, straightforward utility access, and no side that must remain open for service. If it does not affect the surrounding structure and can still reach its final position after most booth elements have been assembled, it remains content inside the booth, not the starting point for the layout.
A heavy unit with several practical positions can therefore be less restrictive than a smaller cabinet with one connection side, one usable access route, and a technical screen that must remain visually connected to it. Size matters when it removes placement options, not simply because the product occupies more floor space.
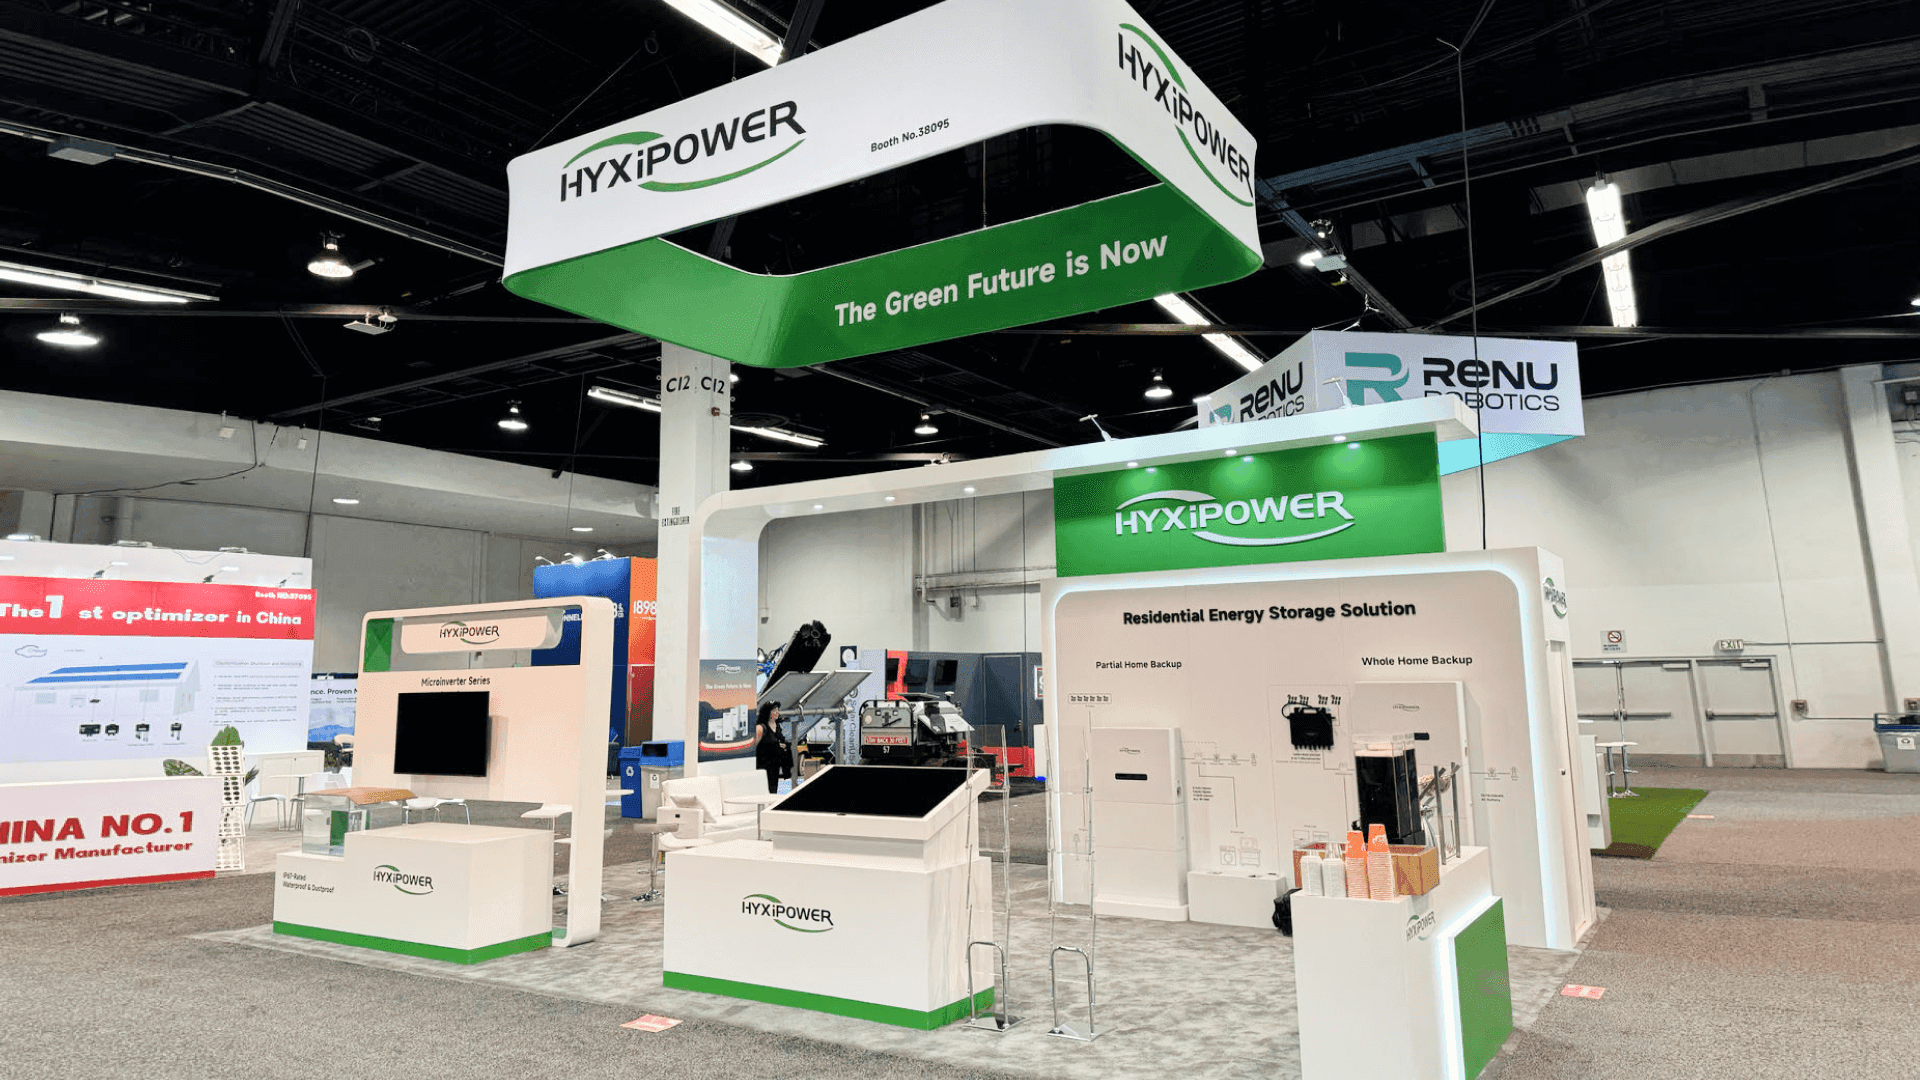
The space around full-size energy equipment can become part of the planning requirement once connections and service access begin limiting nearby booth functions.
The Turning Point Is Loss of Position Flexibility
The first meaningful threshold is reached when equipment can no longer move freely within the floor plan. An inverter cabinet, mixer, conveyor section, or feeder may appear to fit in several locations at first. But connection points, operating clearance, service access, structural support, and the placement of a supporting screen or system diagram can quickly reduce those options.
Once only one or two positions remain workable, walls, counters, screens, storage, and discussion areas can no longer be planned independently. The equipment position has become a design input rather than a decision that can wait until later.
The equipment has shifted from an item placed within the layout to a fixed position that other layout decisions depend on.
Connections and Access Begin to Reserve Nearby Space
The visible outline of a cabinet, processing machine, conveyor module, or feeder does not show every requirement around it. One side may carry power, controls, or product connections, while another may need to remain open for inspection, maintenance, material loading, sample handling, or component removal.
The real question is not the exact clearance measurement, but whether the space beside the equipment remains available for another booth function. If a wall, counter, storage element, or meeting area cannot realistically occupy that space, the equipment is reserving more room than its visible footprint suggests. At that point, the booth is no longer deciding only where the equipment goes; the equipment is beginning to decide what can be built around it.
Landscape machinery and attachments create the same constraint at The Landscape Show. When planning an equipment display booth for The Landscape Show, the working footprint must include room for buyers to walk around the unit, inspect controls or attachment points, and speak with staff without crowding the aisle. A machine may fit on the floor plan but still need to be positioned first when those inspection and access requirements determine where walls, counters, and storage can go.
Screens and System References Can Depend on Product Position
Equipment can bring another dependency into the booth: the physical product may need operating data, samples, controls, or a system-level explanation close enough for buyers to understand what they are seeing. An inverter cabinet may need monitoring information, a processing machine may need input-to-output samples or operating data, and a conveyor, feeder, or valve may need a material-flow diagram showing where the component sits within a larger system.
A screen tied to one machine cannot always be positioned independently. The same applies to a process graphic or an upstream-and-downstream diagram that refers to several physical components. When equipment location, access, screen direction, and the supporting explanation depend on one another, they should be resolved during the booth design and engineering stage, before the surrounding structure limits where either the equipment or its explanation can go.
This does not mean every equipment display needs a complex digital demonstration. The point is that when buyers can understand the product only through a specific relationship between the hardware, evidence, and viewing direction, equipment placement is no longer an isolated decision.
Process Evidence and Material Flow Can Depend on Equipment Position
At The Powder Show, equipment position can determine whether buyers understand what a machine does and how it fits into a larger process. The physical product may be the starting point, but samples, operating data, controls, diagrams, and service access often provide the context needed to evaluate it.
A mixer, mill, dryer, screener, or separator may need input and output samples, operating conditions, process data, or a supporting screen within the same viewing field. A conveyor, feeder, valve, bin, or weighing unit may need an upstream-and-downstream diagram to show how material moves through the wider system.
If those proof elements are separated from the equipment, buyers have to reconstruct the process themselves. The product does not need to tell the entire story on its own, but it does need a position that keeps the relevant evidence and system context close enough to be understood as one technical presentation.
Installation Sequence Can Make Product Position a Design Input
Installation becomes a design issue when equipment must reach its final location before nearby booth elements can be completed. A full-size unit may need a clear route through the booth, which means walls, counters, screens, or finished surfaces may have to wait until the hardware is in place. Product position is then shaping the build sequence, not merely the finished layout.
The same relationship can be seen in HyxiPower’s 20x30 RE+ exhibit, where inverter and residential energy-storage products had to be considered alongside how the exhibit would be packed, delivered, and assembled.
The principle is straightforward: if equipment must be placed before the surrounding build can be completed, its final position has to be known early enough for the structure to accommodate the installation sequence. That also brings freight and pre-show coordination into the process earlier. The critical question is not only when the equipment arrives, but whether the required route remains physically open until the unit reaches the position on which the layout depends.
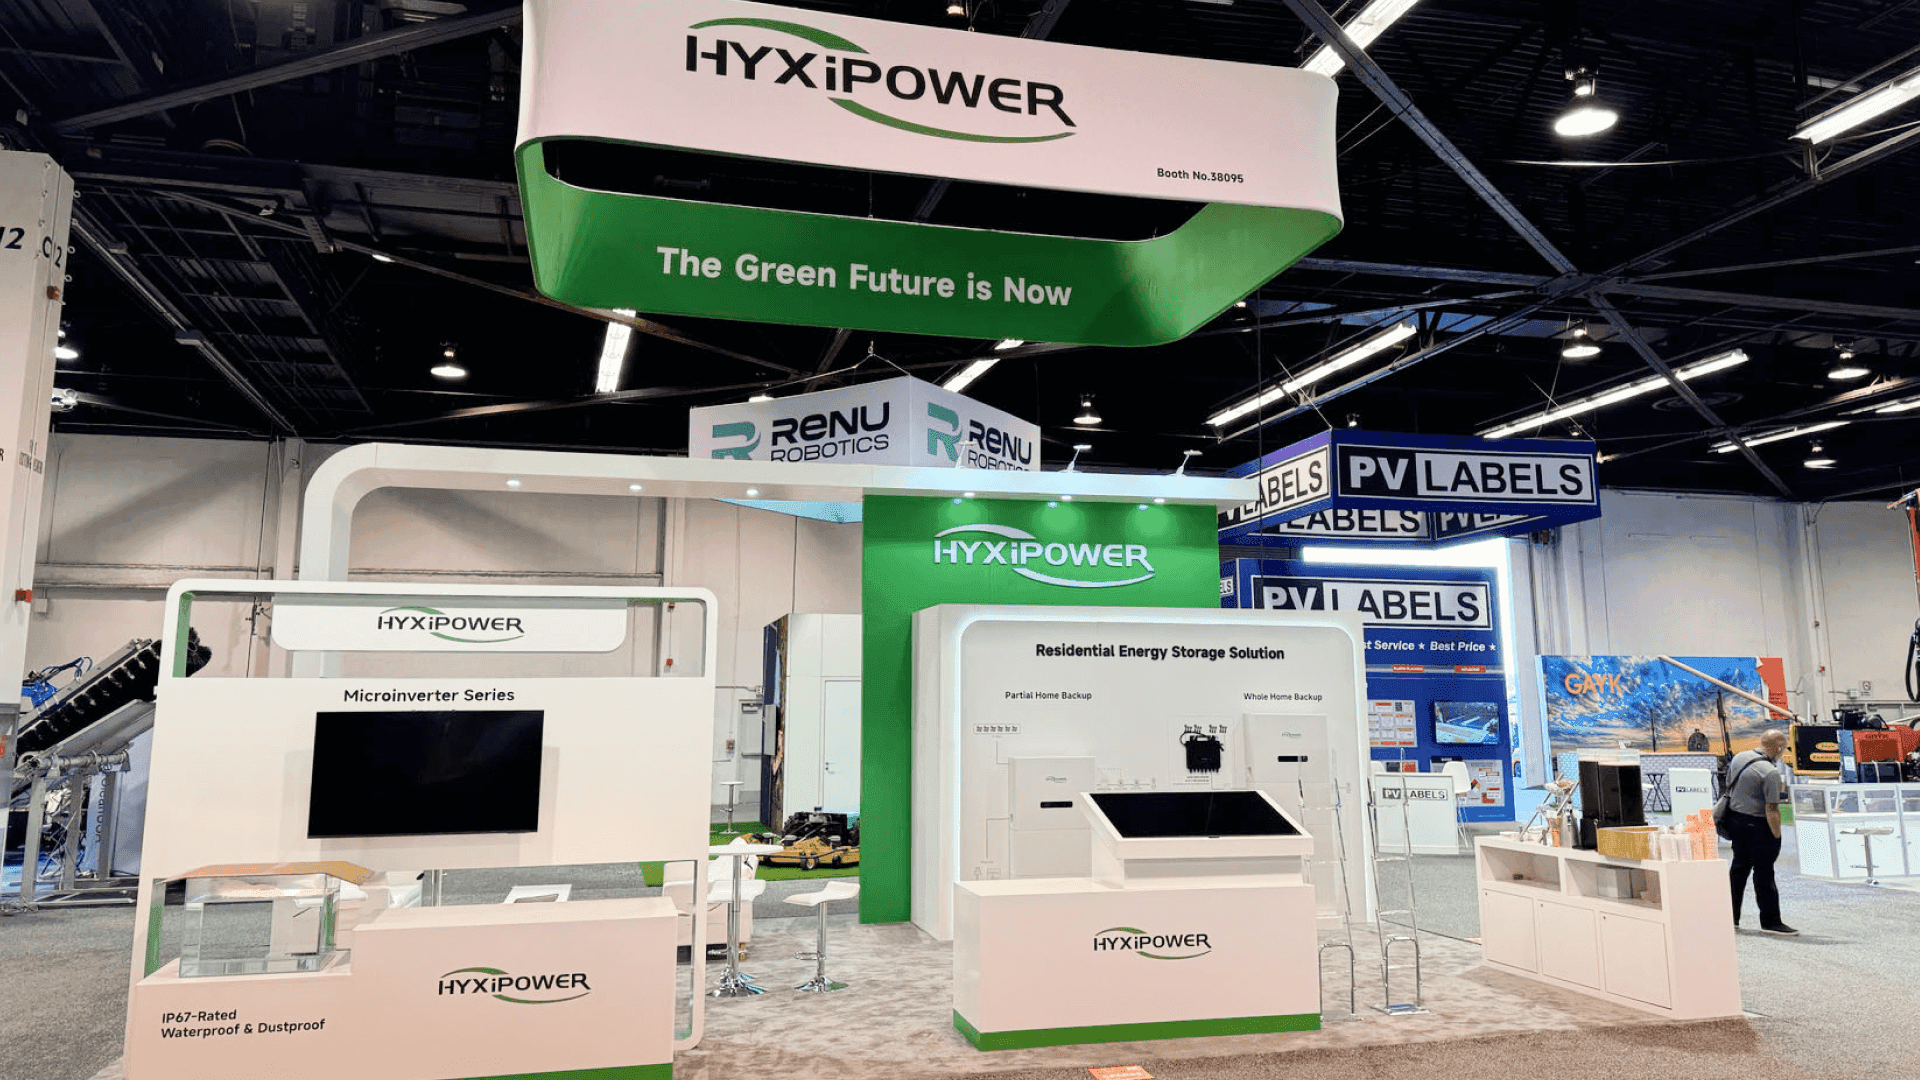
When monitoring data and system graphics need to stay visually connected to the hardware, equipment position becomes part of the technical presentation.
Fix the Equipment First When Multiple Decisions Depend on It
A single requirement rarely changes the entire planning method. A machine may need power, compressed air, material access, or staff clearance and still fit in several workable positions. The threshold becomes clearer when several otherwise separate decisions begin to depend on the same final equipment location.
This threshold appears in industrial exhibits when a processing machine, conveyor section, feeder, control cabinet, supporting display, and installation route all depend on one fixed position. Moving the equipment would then affect not only the floor plan, but also utility routing, service clearance, technical explanation, and show-site setup.
An equipment-first process becomes appropriate when the surrounding structure, utilities, installation sequence, and technical presentation can no longer be finalized independently. At that point, the equipment position and its non-negotiable requirements should be fixed before the surrounding booth layout.
Fix the equipment first when structure, utilities, installation, and technical presentation all depend on its exact position.
What Changes After the Equipment Position Is Locked
Fixing the equipment first does not necessarily make the booth more complex; it moves a few critical decisions earlier. Once the product position is known, structural support, technical displays, utilities, and surrounding booth elements can be planned around it, while freight and placement planning preserve the route needed to bring the equipment into place.
By the time show-site installation begins, the equipment, structure, utilities, and presentation should follow an agreed sequence instead of competing for the same floor space. The booth itself can still remain simple. The difference is that the layout starts with the equipment’s non-negotiable requirements rather than trying to fit the product into an already finished plan.
Dependency Matters More Than Equipment Size
The strongest signal is not equipment size but dependency. When several decisions involving structure, utilities, installation sequence, and technical presentation cannot be resolved without knowing the product’s final location, that location needs to become an early design input.